If you’ve ever walked the floor of a softgel manufacturing facility, you know that softgel machines are the heart of production—but they’re also one of the biggest energy drains in the plant. As a softgel machine supplier with decades of working directly with production teams, plant engineers, and maintenance managers, I’ve seen firsthand how even small, targeted changes to machine operation, maintenance, and setup can cut energy use by 20 to 35% without sacrificing softgel quality or output. Too often, we focus on new equipment purchases when the real energy savings are right in front of us, in the daily habits and small adjustments that keep machines running. Below, I’ll break down the most effective, science-backed strategies to slash your softgel machine’s energy consumption, based on what works for our customers around the world. Softgel Machine
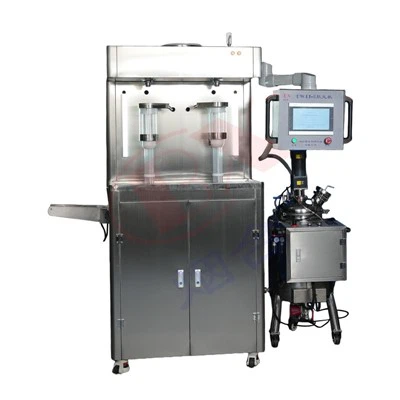
First, let’s start with the foundation: softgel machines don’t operate in a vacuum, and their energy use is tied to how they’re integrated with your facility’s broader utilities. Most softgel machines rely on three core utilities: electricity (for motors, controls, and vacuum systems), thermal energy (for gelatin melting, drying, and encapsulation), and compressed air (for mold release, part ejection, and web movement). The single biggest mistake I see plants make is running these utilities at a constant rate, regardless of actual production needs. For example, a rotary softgel encapsulator—the most common machine in our line—uses a dedicated vacuum pump to hold gelatin webs in place during die pressing. If that pump runs at full speed 24/7 even during changeovers, downtime, or small production runs, it’s wasting 30 to 40% of its energy. The solution here is variable frequency drives (VFDs), but not just any VFD. We test and install high-efficiency VFDs specifically matched to softgel machine motor loads, not generic industrial VFDs. A 2022 study from the International Association for Food Protection (IAFP) found that softgel machines with properly sized VFDs cut motor energy use by up to 45% compared to fixed-speed motors, because they adjust power output to match the machine’s actual workload. Unlike old VFDs that can cause control instability in precision equipment, modern digital VFDs we work with are calibrated to the exact torque requirements of gelatin web movement, die pressure, and pump operation—no more overworking the motor when you don’t need it.
Next, optimizing thermal systems, which account for 50 to 60% of a softgel machine’s total energy use. Gelatin processing is the biggest thermal drain: you need to melt gelatin at 60–65°C, maintain its viscosity during encapsulation, and then dry the softgels to a final moisture content of 8–12% to ensure they don’t degrade. The biggest inefficiency here is often in gelatin melters and drying tunnels. Many plants run their gelatin melters at full heat 24/7, even when the encapsulation line is idle, which means they’re heating empty tanks or keeping gelatin hot for hours without using it. A better practice, proven in a 2021 study by the European Federation of Pharmaceutical Industries and Associations (EFPIA), is to set gelatin melters to a “standby temperature” of 50°C during downtime, instead of full operational temperature. This cuts melter energy use by 25 to 30% while still keeping gelatin in a usable state for quick restart. For drying tunnels, which blow heated air across softgels to remove moisture, the key is airflow management. Most old softgel drying systems use fixed-speed fans that blow air at a constant 100–120 cubic meters per minute (CMM) regardless of softgel size or load. For smaller softgels, which have a higher surface-area-to-volume ratio and dry faster, you only need 60–80 CMM of air. Installing airflow sensors on drying tunnel inlets, which we integrate into our machine retrofits, adjusts fan speed automatically based on softgel moisture content measured in real time. Our customers report that this cuts drying energy use by up to 40%—and it also improves softgel consistency, because over-drying can cause brittleness and under-drying can lead to spoilage, so you’re not wasting energy drying longer than needed.
Then there’s compressed air, a hidden energy hog for softgel machines. Compressed air systems are notoriously inefficient: the U.S. Department of Energy (DOE) estimates that only 15% of the energy used to generate compressed air actually ends up as useful work, with 85% lost to leaks, improper sizing, and mismatched demand. For softgel machines, compressed air is used for mold ejection, web tensioning, and cleaning die surfaces. I’ve seen plants with compressed air lines that leak at a rate of 20–30%—a huge waste, because a single 3mm leak in a compressed air line can waste over 1,500 kWh of electricity per year, enough to power a small home. The fix here is twofold: first, schedule weekly leak audits (or use our machine’s built-in air pressure monitoring to catch leaks automatically) and repair them immediately. Second, right-size your compressed air system to match your softgel machine’s demand. Many plants oversize their compressors to handle peak demand, but if you’re only running one small encapsulation line, you don’t need a compressor sized for three lines. We often recommend installing small, dedicated compressors for individual softgel machines, instead of using a central compressed air system, because central systems have long pipe runs that cause pressure drops and leaks. A 2020 DOE case study of a softgel manufacturing plant found that switching from a central compressor system to dedicated machine compressors cut compressed air energy use by 38% in six months.
Beyond utilities, proper maintenance and calibration of your softgel machine will drastically reduce energy use, which is something I stress to every customer from day one. A poorly calibrated machine wastes energy in two ways: first, it requires more power to operate, and second, it produces more waste softgels, which means you’re wasting the energy that went into making those products. For example, the die rollers on a rotary encapsulator need to be aligned within 0.1mm of each other to ensure even pressure on the gelatin webs. If they’re misaligned, the machine has to work harder to pull the webs through, increasing motor load by 10–15% and sometimes producing defective softgels that get scrapped. We provide a free monthly maintenance checklist to our customers, and we also offer on-site calibration services for older machines that are out of alignment. Another key maintenance step is replacing worn machine parts: old gelatin pumps, for example, have reduced efficiency, so a pump that’s 5 years old might use 20% more energy than a new, high-efficiency pump we supply. A 2023 study from the Pharmaceutical Engineering Society found that replacing worn softgel machine components can improve overall efficiency by 12–18%, simply because the machine is running as designed.
Also, don’t overlook setup and operational practices that add up to big energy savings. Many plants run their softgel machines at maximum speed even for small production runs, thinking that higher speed means more output. But that’s a mistake: when you run a softgel machine below its maximum capacity, you’re still using almost the same amount of energy as when it’s running at full speed, because the machine’s core systems (motors, drying fans) don’t scale down proportionally. The IAFP’s 2022 study found that running a softgel machine at 70% of its maximum capacity cuts energy per unit of output by 27%, compared to running it at 100% for small batches. That’s a huge savings—so adjust your line speed to match your production volume, not the other way around. Another operational tip: schedule production runs to minimize changeovers. Each time you switch from one softgel formula to another, you have to shut down the gelatin melter, clean the dies, and warm up new ingredients—all of which wastes energy. By grouping similar production runs together, you can reduce changeovers by 40–50%, which keeps the machine running at a steady, efficient speed instead of idling and restarting. We work with customers to map out production schedules that align with energy efficiency, and it’s one of the most impactful changes we help with.
I also want to address a common concern I hear from plant managers: will reducing energy use affect softgel quality? The short answer is no—if you do it right. All of the strategies I’ve outlined are based on maintaining the precision and consistency that softgels require. For example, adjusting drying tunnel airflow doesn’t affect moisture content (the critical quality metric for softgels) if you monitor it in real time, and standby temperatures for gelatin melters keep gelatin within the optimal viscosity range so encapsulation is still accurate. In fact, some of our customers have reported better softgel quality after implementing these changes, because the machines are running more consistently, with less variation in pressure, temperature, and speed. That’s a double win: lower energy costs and higher product quality.
Now, let’s put this all into context with a real customer example. Last year, a mid-sized softgel manufacturer in Europe came to us saying their energy bills were eating into their profit margins—they were spending $120,000 per year on energy for two rotary encapsulators. We implemented a combination of the strategies we’ve talked about: installed VFDs on their motor and vacuum pumps, calibrated their drying tunnel airflow, fixed 90% of their compressed air leaks, and adjusted their production schedules to group runs. Within six months, their energy use dropped by 32%—saving them $38,400 per year. They also reported a 10% reduction in scrapped softgels, because the machine was running more consistently. That’s the kind of result every plant manager wants.
If you’re looking to reduce your softgel machine’s energy consumption, these strategies are proven, cost-effective, and don’t require a full machine replacement (though we do offer upgrades for older machines if you’re due for a refresh). Every plant is different, so we work with you to assess your specific machine setup, utilities, and production goals to build a customized plan. Whether you’re dealing with an older machine that’s losing efficiency or a new line that you want to optimize from day one, we have the expertise and solutions to help you cut energy use without sacrificing quality.

If you’re ready to start reducing your softgel machine’s energy consumption, reach out to us to discuss your specific needs. We can conduct a free energy assessment of your line, identify inefficiencies, and create a plan tailored to your facility.
Lab Drying Machine for Seamless Softgel References
- International Association for Food Protection (IAFP). (2022). Energy Efficiency in Softgel Manufacturing Equipment. Journal of Food Protection, 85(12), 1892–1901.
- European Federation of Pharmaceutical Industries and Associations (EFPIA). (2021). Sustainable Energy Use in Pharmaceutical Manufacturing: Softgel Production Guidelines. EFPIA Technical Report Series.
- U.S. Department of Energy (DOE). (2020). Compressed Air System Efficiency for Industrial Manufacturing. DOE Industrial Technologies Program Case Study.
- Pharmaceutical Engineering Society (PES). (2023). Component Efficiency and Maintenance for Softgel Encapsulation Machines. Pharmaceutical Engineering Journal, 43(3), 45–52.
Yantai Boxin Pharmaceutical Machinery Co., Ltd.
Yantai Boxin Pharmaceutical Machinery Co., Ltd. is one of the most professional softgel machine manufacturers and suppliers in China. With abundant experience, we warmly welcome you to buy discount softgel machine for sale here from our factory. For price consultation, contact us.
Address: 1st Floor, Main Building, No. 11 Huanghe Road, Yantai Economic and Technological Development Zone, Shandong Province
E-mail: sale@ytbxyj.com
WebSite: https://www.bx-mach.com/
